 English
 Español
 Português
 русский
 Français
 日本語
 Deutsch
 tiếng Việt
 Italiano
 Nederlands
 ภาษาไทย
 Polski
 한국어
 Svenska
 magyar
 Dansk
 Suomi
 العربية
 ελληνικά
 český


Products
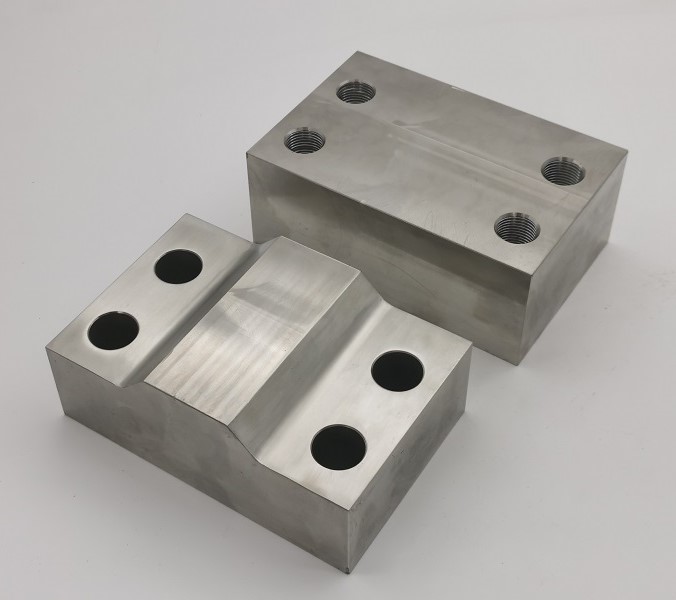


Custom 304 Stainless Steel Split Spider Hub
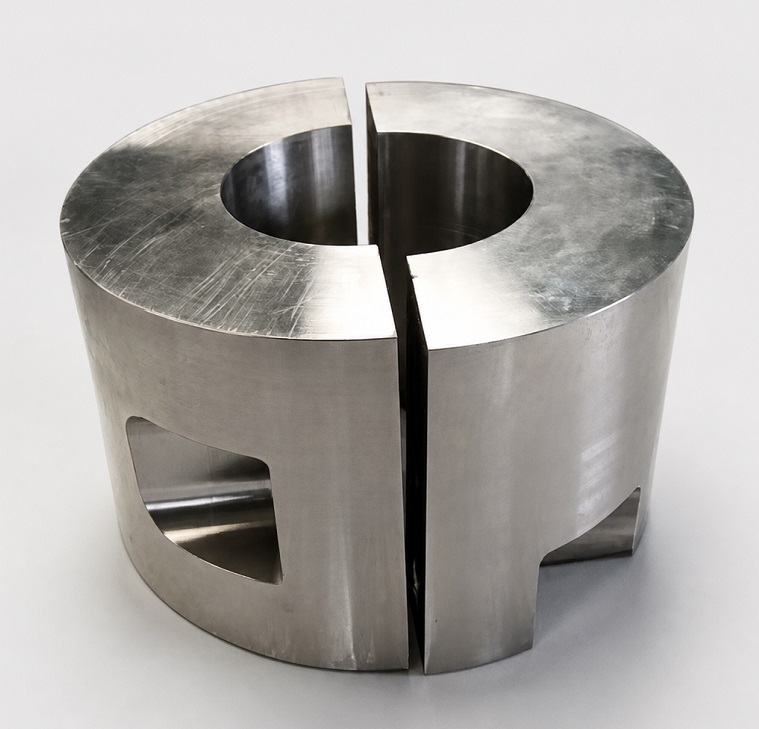
Custom 304 Stainless Steel Split Spider Hub manufactured by JG from 13-inch stainless steel round bar. The hub is completely CNC machined before wire EDM splitting to maintain bore geometry, paired-half alignment and reliable assembly. Large-diameter turning, deep-hole machining, 1-1/4-7 UNC threading and dimensional inspection are controlled throughout production.
Material / Size:
AISI 304 Stainless Steel; OD 13.00 in; Bore 6.25 in; Length 8.50 inProcess / Critical Features:
Large CNC Turning + Milling + Deep Drilling + 1-1/4-7 UNC Tapping + Wire EDM Splitting
Model:AOS05HS32S0001
Send Inquiry
Product Description
Custom 304 Stainless Steel Split Spider Hub
JG manufactures the Custom 304 Stainless Steel Split Spider Hub for heavy-duty industrial clamping, drive and mechanical assemblies. This large hub is machined from solid 304 stainless steel round bar and supplied as a matched two-piece assembly. The manufacturing sequence is critical: all turning, boring, milling, drilling and threading operations are completed while the hub remains whole, and the finished hub is then separated by wire EDM cutting.
Product Overview
The Custom 304 Stainless Steel Split Spider Hub is produced to drawing AOS05HS32S0001. Its nominal finished dimensions are 13.00 inches outside diameter, 6.25 inches bore diameter and 8.50 inches axial length. The component includes two opposed relief windows, stepped side features and paired bolt locations with clearance holes and deep 1-1/4-7 UNC threads.
Manufacturing Process
- 304 stainless steel round-bar verification and sawing
- Large-diameter CNC turning and face machining
- Precision boring of the 6.25-inch central bore
- CNC milling of opposed relief windows and external features
- Deep drilling, counterboring and 1-1/4-7 UNC tapping
- Complete dimensional inspection while the hub is whole
- Wire EDM splitting into two matched halves
- Cut-surface deburring, paired-part identification and final inspection
- Cleaning, corrosion protection and export packaging
Complete Machining Before Wire EDM Splitting
The main engineering value of the Custom 304 Stainless Steel Split Spider Hub is the controlled process sequence specified on the drawing. Machining the bore, outside diameter, faces, windows and bolt features before parting preserves a common centerline and consistent datum relationships. Wire EDM then produces a narrow, controlled split with minimal mechanical cutting force. The two halves remain permanently identified as a matched set.
Large Bore Accuracy and Dimensional Stability
Machining a 6.25-inch bore through a heavy 304 stainless steel hub requires rigid workholding, balanced stock removal and controlled cutting conditions. Heat generation and residual stress can affect roundness and coaxiality, especially when the finished ring is divided. JG applies staged roughing, stress-conscious tool paths, finish boring and inspection before and after splitting to verify that the Custom 304 Stainless Steel Split Spider Hub assembles consistently.
Product Features
- Solid AISI 304 stainless steel construction
- Large 13-inch outside diameter and 6.25-inch precision bore
- Complete CNC machining before separation
- Low-force, narrow-kerf wire EDM splitting
- Matched and traceable hub halves
- Deep 1-1/4-7 UNC internal threads
- Corrosion resistance for demanding industrial environments
- Material certificates and dimensional reports available
- OEM manufacturing according to customer drawings
Applications
- Heavy-duty clamping and shaft assemblies
- Industrial drive systems
- Large processing and handling machinery
- Corrosion-resistant mechanical equipment
- Custom OEM split-hub assemblies
Deep Hole and 1-1/4-7 UNC Thread Machining
The matched fastener system combines top-half clearance holes and bottom-half threaded holes. Drawing features include 1.281-inch diameter holes to a 2.50-inch depth, 1.109-inch tap-drilled holes to a 3.21-inch depth and 1-1/4-7 UNC threads to a 2.50-inch depth. Accurate hole entry, perpendicularity, thread depth and chip removal are essential for smooth bolt engagement and dependable clamping force.
Technical Specifications
| Drawing / Model | AOS05HS32S0001, Revision A |
|---|---|
| Product | Matched two-piece split spider hub |
| Material | AISI 304 stainless steel |
| Raw Stock | 13-inch diameter round bar, approximately 8-3/4 inches long |
| Finished Outside Diameter | 13.00 inches |
| Finished Bore | 6.25 inches |
| Axial Length | 8.50 inches |
| Threads | 1-1/4-7 UNC, 2.50-inch specified depth |
| Parting Method | Wire EDM cutting after complete machining |
| Drawing Weight | Approximately 228.17 lb |
| Inspection | CMM, bore measurement, thread gauges, matched-half fit and visual inspection |
Quality Control
Quality control for the Custom 304 Stainless Steel Split Spider Hub focuses on material traceability, bore size and roundness, outside diameter, face parallelism, hole position, thread depth and paired-half alignment. The internal threads are checked using appropriate gauges, and both halves are assembled after wire EDM cutting to confirm that the bore, outside profile and bolt system remain correctly matched.
Large Stainless Steel CNC Machining from JG
JG supplies the Custom 304 Stainless Steel Split Spider Hub from raw-material procurement through large CNC machining, deep-hole threading, wire EDM parting and final paired inspection. Our process controls the relationships between the bore, outside diameter, mounting holes and split faces, giving OEM customers a reliable matched assembly supported by material and inspection documentation.
Hot Tags: 304 stainless steel split spider hub, custom spider hub, CNC machined split hub, large stainless steel hub, wire EDM split hub, 1-1/4-7 UNC machining, heavy duty clamping hub, OEM CNC machining
Product Tag
Send Inquiry
Please feel free to fill your inquiry in the form below. We will reply you in 24 hours.


X
We use cookies to offer you a better browsing experience, analyze site traffic and personalize content. By using this site, you agree to our use of cookies.
Privacy Policy