 English
 Español
 Português
 русский
 Français
 日本語
 Deutsch
 tiếng Việt
 Italiano
 Nederlands
 ภาษาไทย
 Polski
 한국어
 Svenska
 magyar
 Dansk
 Suomi
 العربية
 ελληνικά
 český


Products
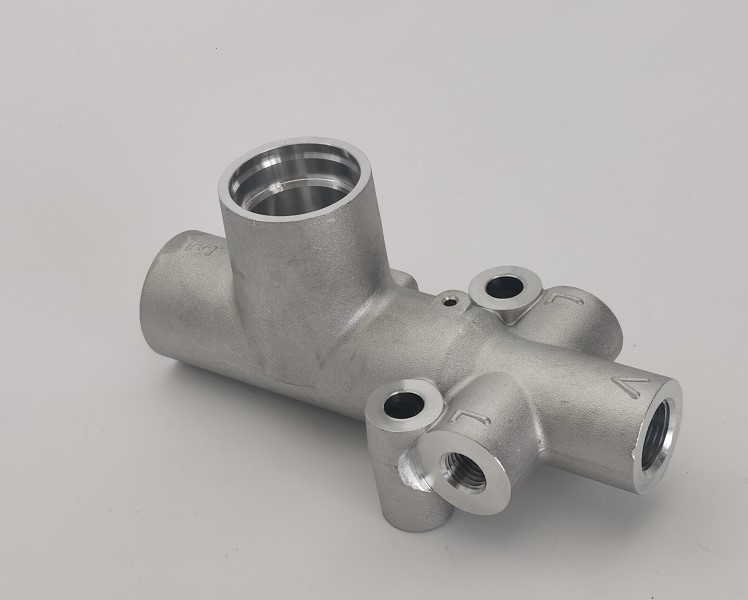
Custom A356-T6 Aluminum Valve Body Casting
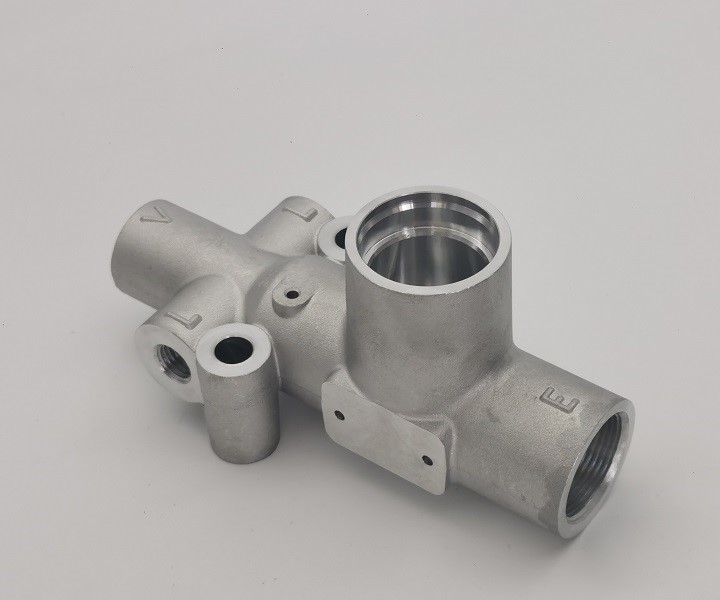
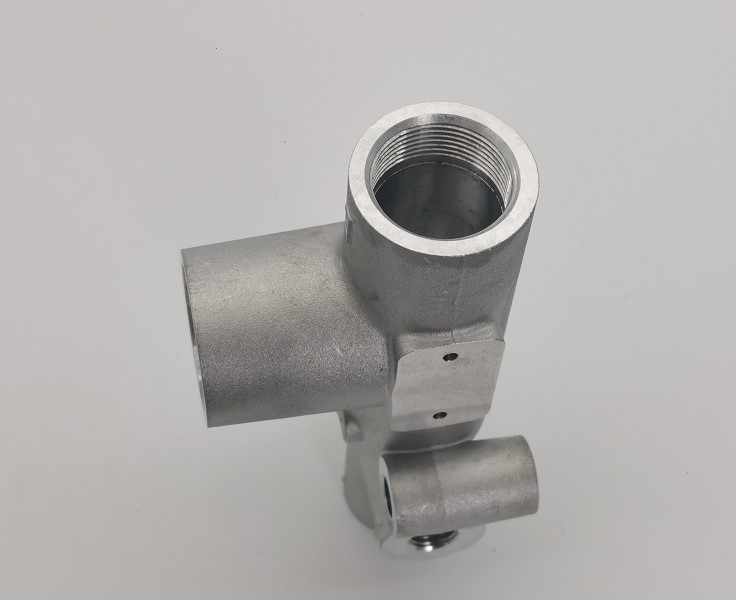
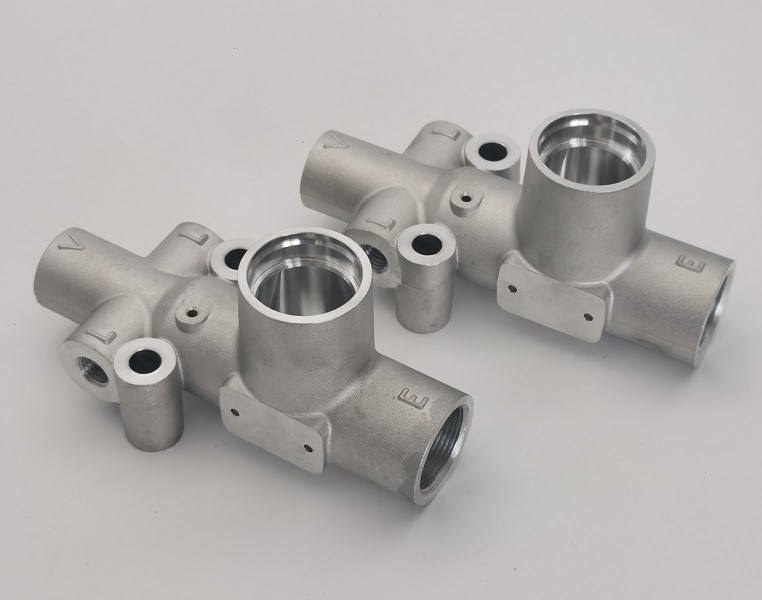
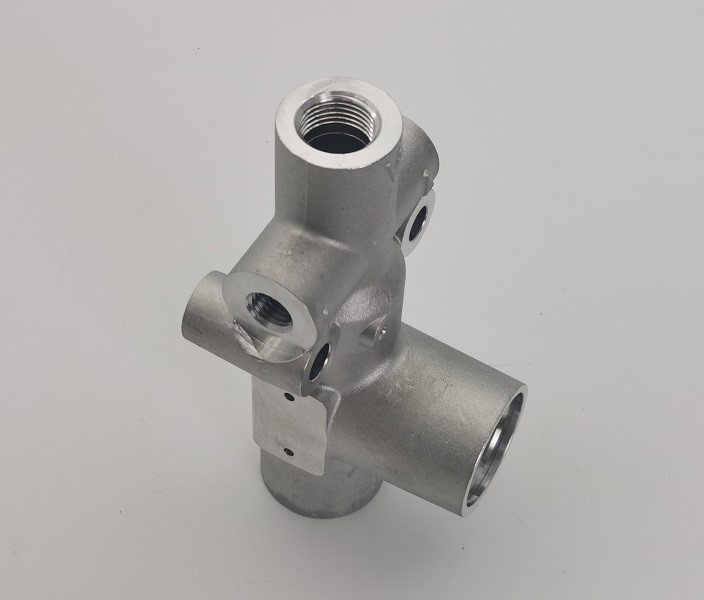
Custom A356-T6 Aluminum Valve Body Casting by JG combines a lightweight multi-port casting with precision CNC bores and threads. Each Custom A356-T6 Aluminum Valve Body Casting is material verified, dimensionally inspected and leak tested at 0.65 MPa for 40 seconds for dependable fluid-control assemblies.
Material / Process:
A356-T6 Aluminum; Casting + T6 Condition + CNC MachiningTesting / Inspection:
0.65 MPa Leak Test for 40 s; Dimensional and Thread Inspection
Model:26-06TT / RUD10951L1
Send Inquiry
Product Description
Custom A356-T6 Aluminum Valve Body Casting
JG manufactures the Custom A356-T6 Aluminum Valve Body Casting for fluid-control, hydraulic and pneumatic equipment that requires a lightweight housing with multiple intersecting passages. The part combines a complex cast shape with accurately machined bores, sealing seats, mounting faces and internal threads. Casting reduces material waste and creates the branched external geometry efficiently, while CNC machining establishes the functional interfaces needed for reliable assembly.
The production version uses A356 aluminum alloy in the T6 condition. Material chemistry is verified by batch, and the finished valve body receives dimensional, thread and leakage inspection. A documented leakage test at 0.65 MPa with a 40-second hold produced zero failures in the tested seven-piece batch, confirming the integrity of the pressure-containing body.
Aluminum Casting and CNC Machining Process
The Custom A356-T6 Aluminum Valve Body Casting begins with controlled aluminum casting to form the multi-branch housing, bosses and internal flow-path geometry. The T6 condition provides a useful balance of strength, dimensional stability and machinability. Machining datums are then established from the casting so each threaded port, precision bore and sealing surface is located consistently.
- A356 aluminum melt and material batch control
- Valve body casting and controlled solidification
- Cleaning, gating removal and surface preparation
- T6 heat-treatment condition verification
- Datum machining and precision fixture setup
- CNC boring, facing, drilling and internal threading
- Deburring and cleaning of intersecting flow passages
- Dimensional, thread and surface-finish inspection
- 0.65 MPa leakage test with a 40-second hold
- Final cleaning, documentation and export packing
Complex Multi-Port Geometry
The valve housing contains several intersecting ports arranged in different directions. This geometry creates two linked manufacturing challenges: maintaining casting integrity around changes in section thickness and accurately locating machined passages from stable datums. Process planning must also provide tool access to internal features without damaging the surrounding cast surfaces.
JG controls fixture orientation and machining sequence so the main bore, side ports, mounting holes and threaded connections remain correctly related. For the Custom A356-T6 Aluminum Valve Body Casting, burr removal is especially important where drilled passages intersect inside the housing. Internal edges are cleaned to support unobstructed flow and prevent loose particles from entering the final system.
Precision Bores, Threads and Sealing Surfaces
The drawing includes a 28 mm H7 precision bore, a 32 mm K7 locating diameter and 26 mm H8 port features. Threaded connections include M28 x 1.5-7H, M18 x 1.5-7H and M12 x 1.5-7H. These features require controlled tooling, rigid workholding and suitable thread inspection to achieve repeatable assembly fit.
Sealing performance depends on more than diameter alone. Bore roundness, coaxiality, face position, chamfer geometry and local surface finish all affect the installed valve components. The Custom A356-T6 Aluminum Valve Body Casting is machined from defined datums and inspected with gauges and coordinate measuring equipment selected for each critical characteristic.
Leakage Testing for Pressure Integrity
Every pressure-containing valve body requires confirmation that the casting and machined interfaces are leak tight. The documented production test applies 0.65 MPa pressure and holds the pressure for 40 seconds. The referenced batch contained seven valve bodies, with zero failures and an overall result of OK.
Leakage testing helps identify porosity, incomplete sealing, damaged threads or passage defects that may not be visible during ordinary dimensional inspection. Test conditions and acceptance results can be recorded for production traceability. This verification gives OEM customers additional confidence in the Custom A356-T6 Aluminum Valve Body Casting before it enters final equipment assembly.
A356-T6 Material Verification
The actual production material is A356-T6 aluminum. A batch chemical analysis confirmed 7.001% silicon, 0.085% iron, 0.024% copper, 0.015% manganese, 0.334% magnesium, 0.012% zinc and 0.119% titanium, with an overall result of OK. The alloy provides good castability, corrosion resistance and machinability for complex pressure housings.
Material certificates identify the drawing reference, report number and furnace batch for traceability. Combining chemistry verification with process and inspection records helps JG maintain consistent material control from casting through final shipment.
Technical Specifications
| Product | Custom A356-T6 Aluminum Valve Body Casting |
| Model / Reference | 26-06TT / RUD10951L1 |
| Material | A356-T6 Aluminum |
| Manufacturing Process | Aluminum Casting + T6 Condition + CNC Machining |
| Approximate Overall Length | 142 mm reference |
| Overall Width | 60 mm |
| Precision Main Bore | 28 mm H7 |
| Locating Diameter | 32 mm K7 |
| Port Bore | 26 mm H8 |
| Internal Threads | M28 x 1.5-7H; M18 x 1.5-7H; M12 x 1.5-7H |
| Surface Roughness | Ra 3.2 general; Ra 0.8 on specified precision surface |
| Leak Test | 0.65 MPa for 40 seconds |
| Inspection | Material, dimensional, thread, surface and leakage inspection |
Surface Finish and Deburring
The product intentionally combines uniform as-cast surfaces with bright machined interfaces. Functional faces and bores are machined only where accuracy or sealing is required, preserving the material and cost advantages of casting. Machined areas are checked for chatter, tool marks, dents and other defects that could affect assembly.
Intersecting holes, thread entries and internal passage edges are carefully deburred. The completed Custom A356-T6 Aluminum Valve Body Casting is cleaned to remove chips and residue before leakage testing, helping protect downstream valves, seals and fluid circuits.
Quality Control and Documentation
Quality planning covers incoming material verification, first-piece inspection, in-process checks and final functional testing. Calipers, micrometers, bore gauges, thread gauges, height gauges and CMM equipment are used according to feature type and tolerance. Critical sealing and locating dimensions receive focused inspection.
Material certificates, dimensional inspection results and leakage testing records are available for traceability. The documented material report confirms A356-T6 chemistry, while the leakage report records test pressure, hold time, quantity and acceptance result. These records support OEM approval and repeat-order consistency.
Product Features
- A356-T6 aluminum construction for low weight and corrosion resistance
- Complex multi-port valve body casting
- Precision CNC machined bores and sealing surfaces
- M28, M18 and M12 internal threaded connections
- H7, H8 and K7 controlled fits
- Clean, burr-free intersecting internal passages
- 0.65 MPa leakage testing with a 40-second hold
- Material chemistry and furnace-batch traceability
- Inspection documentation available
- OEM manufacturing according to customer drawings
Applications
- Hydraulic valve and manifold assemblies
- Pneumatic control equipment
- Industrial fluid distribution systems
- Automation machinery
- Mobile and material-handling equipment
- Custom OEM pressure-control assemblies
OEM Aluminum Valve Body Manufacturing from JG
JG supplies custom aluminum castings that combine near-net-shape production with precision CNC machining and functional testing. Engineering review covers casting geometry, machining datums, thread standards, tolerance stack-up, internal passage cleaning and leakage-test requirements before production begins.
Send JG your drawing, 3D model, annual quantity and quality-document requirements for a quotation. JG can manufacture the Custom A356-T6 Aluminum Valve Body Casting and similar leak-tested aluminum housings for prototype, small-batch and repeat OEM production.
Hot Tags: A356-T6 aluminum valve body, cast aluminum valve body, CNC machined valve housing, leak tested valve body, custom aluminum casting, hydraulic valve body, pneumatic valve housing, OEM aluminum casting
Product Tag
Send Inquiry
Please feel free to fill your inquiry in the form below. We will reply you in 24 hours.



X
We use cookies to offer you a better browsing experience, analyze site traffic and personalize content. By using this site, you agree to our use of cookies.
Privacy Policy